
Intralogistics: The Word Behind Every Warehouse Project
The word appears in vendor decks, job titles and tender documents, and almost nobody stops to define it. Intralogistics is the discipline of moving, storing and controlling material inside a single facility, from goods-in to dispatch. It is not a product category and not a synonym for automation. It is the engineering and planning work that decides what material has to do inside your four walls, and at what rate.
Equipment sits downstream of that. Shuttles, lifts, conveyors and racking are answers to questions the discipline asks first. Buy the hardware before the analysis and you are guessing.
What follows is a working definition, the boundary lines against neighbouring terms, the equipment and software layers that make up a system, and the numbers material handling projects are actually judged on.
What Is Intralogistics, in Plain Terms?
Intralogistics is the planning, execution and control of material and information flow inside the four walls of a plant, warehouse or distribution centre, from goods receipt through to despatch. It covers how goods move, where they are held and how the data governing both is captured and acted on. That is the intralogistics meaning in one sentence.
The three things intralogistics always covers
Movement comes first: conveyance, transfer, picking and loading. Storage comes second: buffering, sequencing and density in racking, shelving or an automated grid. The third element, data, is the one most buyers underweight, because without accurate location and inventory records the first two degrade into expensive guesswork.
Where the discipline starts and stops
The boundary is the dock door in both directions. Transport between sites belongs to logistics; what happens between unloading and reloading belongs to intralogistics. That scope is why the term sits upstream of equipment choice, and why it is worth separating from what warehouse automation actually means.
Why the word exists at all
The term grew out of German engineering practice and is promoted by bodies such as the VDMA intralogistics association. Europe and Asia use it routinely in specifications and tenders. North America largely kept the older label, material handling, which describes equipment rather than internal logistics as a discipline.
Intralogistics vs Logistics, Supply Chain and Material Handling
Where logistics ends and intralogistics begins
Logistics and supply chain management govern movement between sites: carriers, freight rates, inbound schedules, network design, supplier lead times. Intralogistics starts when a trailer backs onto a dock door and ends when the next one pulls away. Everything in between, receiving, putaway, storage, replenishment, picking, consolidation and dispatch staging, sits inside its scope. The boundary matters commercially, because a transport problem and a throughput problem demand entirely different capital decisions.
Is internal logistics the same thing?
In practice, yes. Many organisations, particularly European manufacturers, say internal logistics where others say intralogistics, and the terms are interchangeable in tenders and job titles. Production logistics is the narrower manufacturing subset: line feeding, kitting, work-in-progress buffering and the timed delivery of components to assembly stations.
Material handling: equipment, not discipline
Material handling describes hardware, conveyors, cranes, shuttles, lifts, AGVs. Intralogistics describes the system those machines serve and the performance it must deliver. Buying equipment without defining the system is how warehouses end up with fast machines and slow operations.
Material Flow Management Is the Core Skill
Intralogistics is flow design first and hardware second. Most projects that underperform were not sold the wrong machine, they were sized against the wrong demand profile. Material flow management is the discipline that prevents this, and it follows a strict sequence before any equipment specification is written.
What a material flow analysis actually measures
- Order profiles: lines per order, units per line, and the share of single-line orders
- SKU velocity: which items generate movements, measured over at least twelve months of order data
- Throughput in units the equipment understands: pallets per hour inbound, totes per hour to pick stations, lines per picker-hour at the face
Why peak hour, not daily average, sizes the system
A facility averaging 120 pallets per hour may need 260 during the pre-cutoff window. Size to the average and the system clears the backlog after the trucks have left. Peak hour, peak day and peak season each produce a different number. All three belong in the specification.
Buffers: the handoffs that decide throughput
Throughput dies at transitions. Calculate dwell time at every buffer position between shuttle, lift and conveyor. If dwell exceeds the arrival interval, the buffer becomes the constraint regardless of shuttle speed.
The Equipment Layer: What Sits Inside an Intralogistics System
Hardware sits downstream of the flow design, not ahead of it. The useful way to read the equipment market is by degree of integration: how tightly a machine is bound to a fixed path, a fixed rack, or a fixed sequence. The looser the binding, the easier it is to change later and the less density you get.
Floor-level transport
- Manual pallet trucks and reach forklifts: move pallets anywhere, good at low volume and unpredictable work.
- AGVs and AMRs: move pallets, totes or carts along the floor, good at linking distant process points without construction.
Storage and retrieval inside the rack
- Vertical lift modules: move small parts in trays, good at recovering floor space for slow movers.
- Stacker-crane ASRS: one machine per aisle serving pallets or totes, good at deep buffering with modest cycle counts.
- In-rack shuttle systems: carriers running inside the rack grid with lifts at the aisle face, chosen when storage density and sustained throughput outrank layout flexibility.
Picking and sortation equipment
- Conveyor and sortation: move cases and polybags along fixed routes, good at high repeatable volume. See our breakdown of warehouse robotics and the wider types of warehouse automation.
The Software Layer: How Intralogistics Is Actually Controlled
WMS, WES and WCS: who decides what
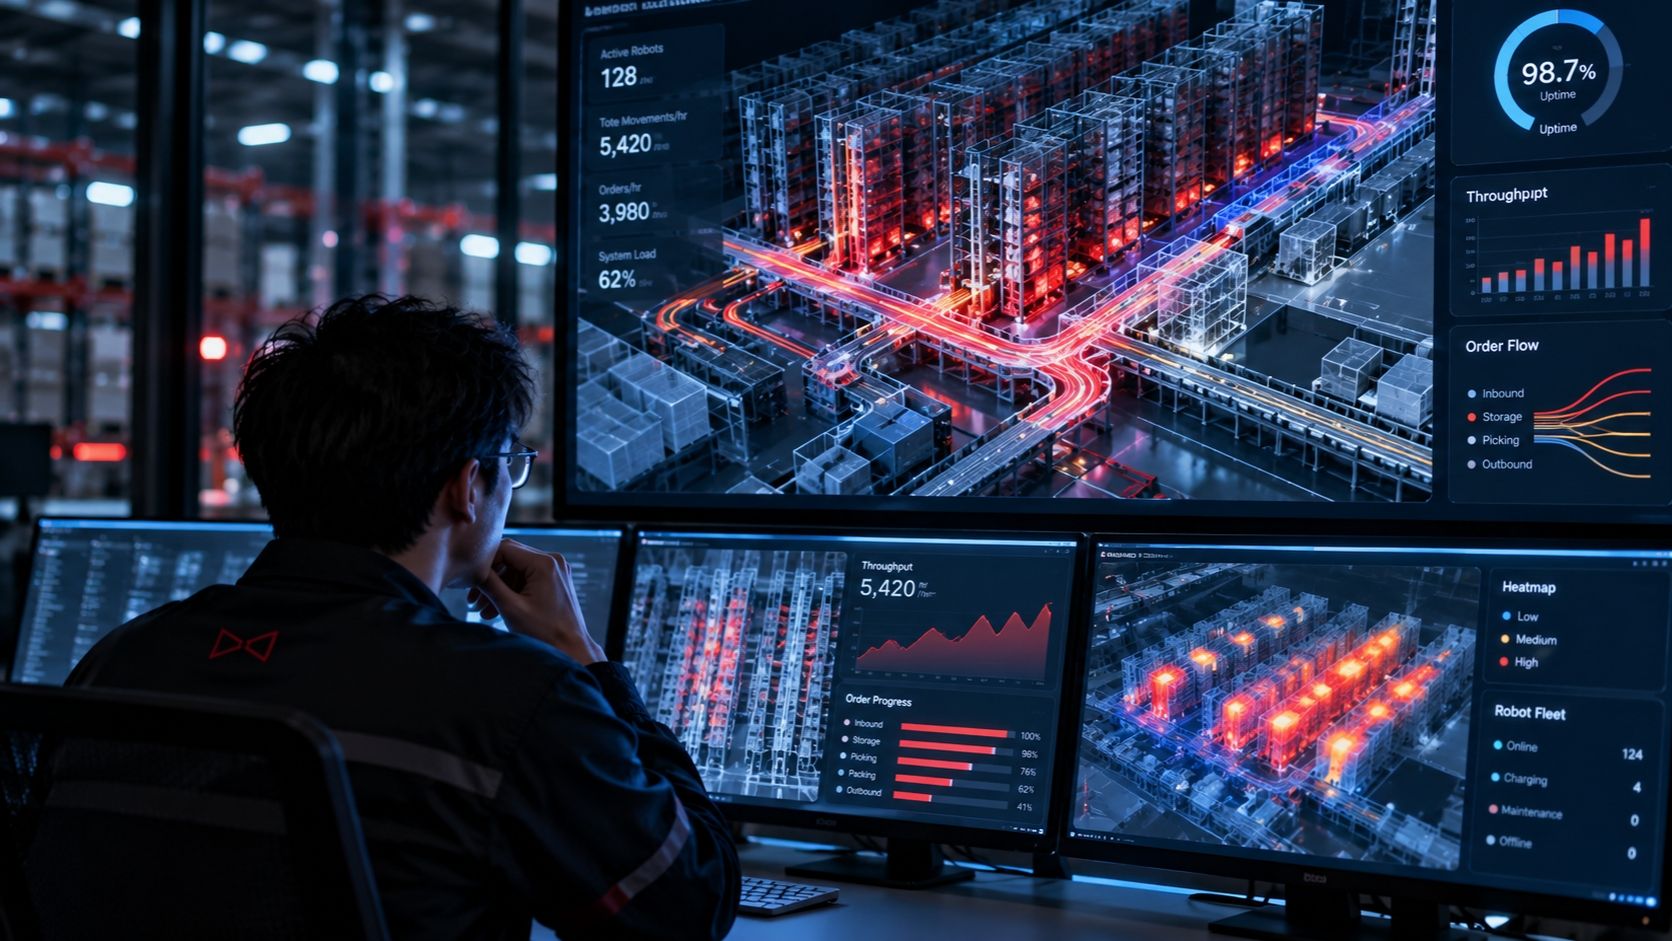
Four layers divide the decisions. The WMS owns inventory records and order logic: what to pick, from which stock, in what sequence of orders. The WES sequences and optimises work across subsystems, balancing shuttle, lift and pick station demand. The WCS talks to machines in real time, issuing move commands and handling traffic. Below that, PLC controllers and device firmware execute motion. Our breakdown of warehouse control system vs WMS and WES maps the boundaries in detail.
Where integration projects go wrong
Failures come from overlap, not absence. Two systems both claiming authority over location assignment produce double-allocated slots. A WMS releasing orders in receipt order rather than by aisle starves lifts while shuttles queue. Pickers stand idle because nobody sequenced totes to arrive in presentation order.
Why software caps throughput before hardware does
Steel has a mechanical ceiling. Software decides how close you get. In automated facilities, poor task allocation and release logic routinely leave mechanical capacity unused, which is why control architecture belongs in the specification, not the commissioning phase.
How Intralogistics Performance Gets Measured
Intralogistics systems are judged on a small set of measurable outputs, not on equipment specifications. These are the metrics practitioners use in design reviews and acceptance testing, each with the unit it is normally reported in.
| Metric | Unit | What it tells you |
|---|---|---|
| Throughput | Pallets or totes per hour | Sustained movement capacity |
| Storage density | Pallet positions per m² or m³ | How hard the building works |
| Order accuracy | % | Quality of execution |
| Dock-to-stock time | Minutes or hours | Inbound responsiveness |
| Picking rate | Lines per hour | Labour and pick-face efficiency |
| Availability | % uptime | Reliability under load |
| Energy per move | kWh | Operating cost per transaction |
Read these together. Throughput measured without availability flatters a system, and density gains mean little if dock-to-stock time degrades. Our breakdown of warehouse KPIs worth tracking explains how to weight them per site.
Why Intralogistics Became a Board-Level Topic
What changed in order profiles
Orders got smaller and more frequent. A pallet-out operation moving full layers to a handful of retail accounts has a different physics problem than one shipping single-line parcels every few seconds. Add SKU proliferation, where ranges expand faster than floor space, and the old answer of more racking plus more pickers stops scaling.
Labour and rent as the twin pressures
Picking roles carry high turnover, and warehouse labour statistics show persistent recruitment difficulty in the sector. Industrial rent per square metre pushes operators to build upward instead of outward. That is why dense in-rack warehouse automation solutions get board attention: they deliver repeatable throughput, fewer handling errors and safer work without acquiring land. The honest trade-off is capital cost and reduced layout flexibility. Steel and rails commit you to a flow pattern for years.
What the next five years look like
Simulation before steel, so throughput is proven in a model first. Modular systems that add shuttles rather than rebuild aisles. Control software that reschedules work dynamically as order mix shifts through the day.
Intralogistics FAQs
1. Is intralogistics the same as warehouse automation?
No. Automation is one option within intralogistics. The discipline covers layout, flow design, labour planning and control logic, whether the work is done by conveyors, shuttles, forklifts or people with scanners.
2. Does a manual warehouse have intralogistics?
Yes. Every facility that receives, stores and ships goods has internal material flow. In a manual site that flow is governed by racking layout, pick paths and process discipline rather than by machines.
3. What background do intralogistics roles need?
Industrial engineering, operations management and supply chain programmes are the common routes, often alongside industrial engineering coursework. Data literacy matters more than brand familiarity, since most decisions rest on throughput modelling and cost per unit handled.
4. Who owns intralogistics, operations, engineering or IT?
Operations owns the performance outcome, engineering owns the physical design and IT owns system integration. Projects fail when no single accountable owner coordinates all three from concept through commissioning.
Start With the Flow, Then Choose the Steel
Intralogistics is a design discipline first and a shopping list second. Shuttles, lifts and conveyors are outputs of a flow decision already made, not substitutes for making it. Buyers who invert that order end up owning hardware that performs exactly as specified against the wrong demand profile.
The useful sequence is unglamorous. Define order profiles by line count and unit type. Establish peak-hour volumes, not annual averages, because peak is what sizes the system. Set a storage density target tied to your building footprint and lease horizon. Decide which decisions belong to software and which to steel. Only then does a vendor shortlist mean anything.
If you are at the flow definition stage, our engineers are glad to talk through throughput and density requirements before any equipment gets named.