
The Pick Station Is Where the Business Case Lives
In a conventional manual operation, roughly half to sixty percent of a picker’s shift is spent walking, not picking. That is the uncomfortable arithmetic behind every peak season hiring plan: once aisles congest, adding headcount stops adding throughput and starts adding interference. A goods to person system attacks the travel directly, bringing inventory to a stationary operator, but the investment is not judged by the concept. It is judged at the workstation, in picks per operator-hour, sustained through a four-hour peak rather than measured in a vendor demo.
What decides whether that rate holds is the storage architecture feeding the station, not the station itself. This article works through the numbers that matter to fulfilment managers and operations directors: realistic pick rates, storage density per square metre, ergonomic design limits, and where the capital actually goes.
What a Goods to Person System Actually Changes
A goods to person system inverts the picking relationship. Storage automation retrieves the SKU carrier, whether tote, tray, case or pallet, and presents it at a fixed station built around the operator’s reach envelope. The operator stays put and the inventory travels. Three things change as a result: travel disappears, accuracy is enforced by the control system, and throughput scales with station count rather than headcount.
Goods-to-person versus person-to-goods
In person-to-goods picking, the operator walks or rides to the location, and travel consumes the majority of the shift. Across most conventional order picking methods, adding volume means adding people and aisle congestion. An automated picking system breaks that link by moving the carrier instead.
What the operator sees at the station
One carrier, one lit location, one confirmed quantity. The sequence is dictated by software, not by memory or a paper list, which is why ergonomic workstation design matters more than pick speed alone.
Why the label alone tells you nothing
Goods-to-person is a presentation strategy, not a single machine. Two systems carrying the same label can differ by a factor of three in output, depending on retrieval device, buffering and station design.
Four Back-End Architectures That Feed a Pick Station
The station sets the ceiling on operator output. The storage engine behind it decides whether that ceiling is ever reached. Four architectures compete for the job, and their operating envelopes differ more than vendor brochures suggest.
Carousels and vertical lift modules
- Horizontal and vertical carousels: typically 25 to 50 kg per carrier location, one retrieval sequence at a time per unit, and usable height limited by ceiling clearance in a single enclosure. Throughput per machine is fixed, so SKU growth means slower rotations and longer operator waits.
- Vertical lift modules: heavier trays, often several hundred kilograms, with excellent density per square metre of floor. But a single extractor serves the whole column, so retrieval rate per machine stays flat no matter how many trays you add. Reference material on vertical lift modules confirms the single-extractor constraint.
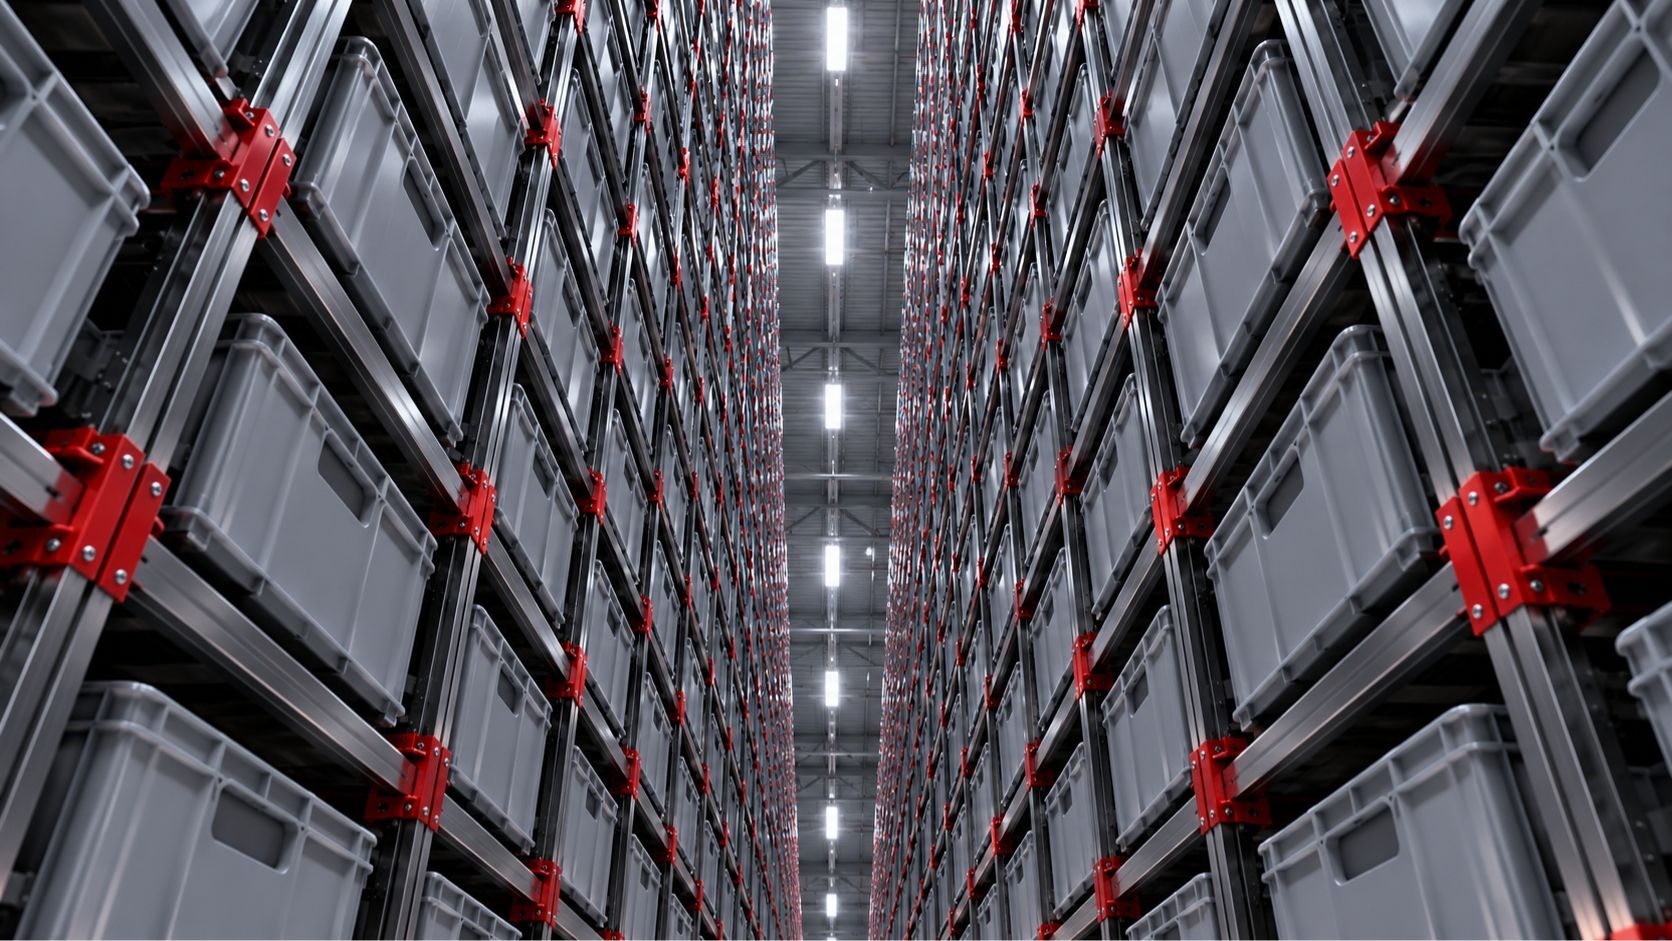
- In-rack tote shuttle and mini-load ASRS: commonly 30 to 50 kg per tote, double-deep or multi-deep storage, and usable height running to the full rack structure. A tote shuttle system adds retrievals per aisle per hour by adding shuttles and lifts, not buildings.
- Robot-carried shelves and totes: flexible and quick to deploy, but density suffers because robots need floor aisles, and usable height is capped by what a mobile unit can lift safely.
In-rack tote shuttle grids
The scaling logic is the dividing line. Carousels and lifts scale by buying more machines and more floor. A shuttle-and-lift grid scales inside the same rack footprint, which is why a gtp system built on in-rack hardware holds its cost per pick as SKU count climbs.
Operator Pick Rates: What the Numbers Really Look Like
Manual baseline versus station output
Manual picker-to-part operations are commonly published in the range of 60 to 120 lines per operator-hour, with travel consuming most of the shift. Single-tote goods to person picking stations are typically quoted in the 200 to 400 picks per hour band. Multi-tote presentation combined with put-wall style batching and a buffered queue is quoted as high as 600 to 1,000 picks per hour, but only where line profiles are small and cartonisation logic is simple.
What pushes a station past 400 picks per hour
Five variables move a station between those bands: how many totes are presented simultaneously, lines per order, the scan and confirmation method (barcode scan, pick to light, or weight check), item weight and grip difficulty, and batch depth. Heavy or awkward items and multi-scan confirmation can cut a station’s rate in half, regardless of how much warehouse throughput the back-end shuttle system can deliver.
Peak rate against sustained shift rate
Treat every quoted figure as a peak number until proven otherwise. The only rate that matters commercially is sustained output measured across a full shift, including breaks, replenishment gaps, short-cycle starvation and exception handling. Ask vendors to state the measurement window. Peak rates sustained for ten minutes do not size a labour plan.
Architecture, Pick Rate and Density Side by Side
The four architectures diverge most where it matters: what one station can sustain, and what the rack behind it costs in cubic metres.
| Architecture | Picks per operator-hour | Retrievals per hour | Density vs selective racking | Usable height | Best-fit SKU count |
|---|---|---|---|---|---|
| Tote shuttle (one level per aisle) | 300 to 500 | 500 to 1,000+ per aisle | 2x to 4x | Up to ~25 m | 10,000 to 100,000+ |
| Roaming/multi-level shuttle | 250 to 400 | Variable by fleet size | 2x to 3x | Up to ~15 m | 5,000 to 50,000 |
| Cube storage | 150 to 300 | Variable by robot count | 3x to 5x | Up to ~12 m | 10,000 to 60,000 |
| Mobile robot (rack-moving) | 200 to 350 | Variable by fleet size | 1.5x to 2x | Floor level only | 5,000 to 30,000 |
Density and station rate rarely peak together. Cube systems win cubic efficiency but constrain presentation sequence; tote shuttles with dedicated levels hold the highest sustained rates. Figures are typical published ranges and must be confirmed by simulation against your own order profile.
Ergonomics: The Reason Rates Hold After Hour Six
Quoted pick rates are measured in the first hour. What matters commercially is the rate in hour seven, and that is decided by station geometry, not by scheduling logic. If the operator has to bend, stretch or twist to reach the tote, the cycle gains a second or two, and fatigue compounds that loss through the shift.
The presentation window that matters
- Present totes between roughly 750 mm and 1,350 mm from the floor, the band where manual handling risk stays lowest.
- Tilt the tote toward the operator and allow height adjustment per user, not per station.
- Keep horizontal reach under 500 mm so no pick requires torso rotation.
- Use pick-to-light plus scan confirmation so the eyes never leave the work zone.
- Offer sit-stand operation; seated picking suits long shifts on small items.
- Control noise and air temperature at the station, not just in the aisle.
Ambient stations in chilled and frozen sites
In frozen operations the grid can run at -25 °C while operators work at ambient. That removes rotation limits, suit changes and the recruitment penalty that defines cold-store labour.
Designing for temporary peak staff
Good geometry shortens training to minutes, lowers injury and absenteeism exposure, and makes peak agency labour productive on day one rather than day three.
Keeping the Station Fed: Density, Buffering and Dual-Cycling
The station rating is a ceiling, not a forecast. What the operator actually achieves is set by retrievals per hour per station, and that number is produced by the storage system, not by the workstation vendor’s spec sheet. Specify the back end against the station and the mismatch becomes obvious before the capital is committed.
Retrievals per hour per station
In-rack shuttle-and-lift architecture separates horizontal and vertical movement, so a shuttle works its tier while the lift works the face. Both devices dual-cycle, pairing a putaway with a retrieval on a single trip, which roughly halves empty travel per presentation. Floor-robot fleets cannot do this at the same scale. Every presentation is a full round trip from grid to station and back, and the fleet size needed to sustain a high-rate station climbs faster than most business cases assume.
Why sequencing buffers decide sustained output
Sustained output depends on the queue in front of the operator. A buffer holding several totes per station absorbs retrieval variance, and conveyor-based sequencing lets the control system fix digging reorders before the tote arrives. Without that depth, one deep retrieval stalls the line.
Aisle-free grids versus robot travel lanes
Robot lanes consume floor area that stored product could occupy. A compact grid raises tote positions per square metre, and high density storage plus velocity-based slotting keeps fast movers near the lift in any goods to person warehouse.
Cost per Pick, and When the Model Does Not Pay Back
Most capital requests for a goods to person system fail review because they compare a quoted price against a forklift fleet. That comparison is meaningless. The only number that survives finance scrutiny is cost per pick over the full asset life.
What sits in the capital number
Five cost blocks drive the quote: the rack grid and its structural steel, the shuttle and lift fleet, the pick stations themselves, the conveyor or transfer decks linking storage to stations, and the control software layer. Fleet size and station count move with throughput, while the grid moves with storage volume, so two systems with identical price tags can hold very different capacity. Then add recurring spend: preventive maintenance, a critical spares holding, drive and charging power, and WCS support or licensing. Ignoring the software line is the most common modelling error we see.
Modelling cost per pick, not cost per station
Build a seven to ten year model. Divide total cost of ownership by cumulative picks, where picks come from station count multiplied by sustained rate multiplied by productive hours per shift multiplied by shifts worked. A second shift roughly halves cost per pick without touching capital, which is why shift pattern matters more than equipment discount. Apply a discounted cash flow view and compare the result against your current fully loaded labour cost per pick. Our note on warehouse automation ROI sets out the input structure.
Profiles where manual picking still wins
Low order volumes, full-pallet or full-case despatch, items beyond tote payload, volatile SKU ranges in short-lease buildings, and sites where a well-slotted pick-to-light zone deploys faster and cheaper.
Common Questions From Operations Teams
1. How many pick stations do I need for a given daily line volume?
Divide daily lines by sustained station rate, then by productive hours, and add 15 to 25 percent headroom for peak-hour skew. Most operations size stations on the busiest hour, not the daily average, because the daily average understates demand by a wide margin in seasonal profiles.
2. What order volume justifies the investment?
The threshold is driven by labour cost and shift count more than by volume alone. Sites running two or three shifts with persistent recruitment difficulty reach payback at lower volumes than single-shift sites with cheap labour.
3. How long does a deployment take from order to go-live?
Expect several months from contract to commissioning, with software integration and site acceptance testing usually the longest poles rather than mechanical installation.
4. What happens to throughput if the system goes down mid-shift?
Partial degradation is normal: aisles and lifts fail independently, so you lose a share of capacity, not all of it. Keep a manual pick fallback for your top-moving SKUs.
Specify the Station, Then the Storage Behind It
The sequence matters more than the equipment list. Fix the sustained picks per operator hour your order profile demands, net of fatigue and short lines, then work backwards to the retrievals per hour and buffer depth required to keep that station from ever waiting. Only at that point does the storage architecture become a real decision rather than a preference. Get the order wrong and you buy robots to feed a station that was never specified.
Remember the structural difference. In-rack shuttle systems buy density and throughput together, because adding levels and lifts adds both. Floor-robot layouts trade one against the other, and that trade shows up in cost per pick long before it shows up in a layout drawing.
Before capital commitment, run a throughput and density review against your own order lines. We are happy to model it with you.